What Causes Uneven Button Feedback in Custom Silicone Keypads for Industrial Weighing Scales?
A bench scale makes a simple promise: put the load on, press Enter, read the number. When the Enter key needs a second, harder push while Tare two centimetres away answers a light touch, operators stop trusting the instrument. They press with the side of a thumb, then with two hands, then they call service. In most of the keypads we pull apart, the electronics are fine. Twelve keys were drawn as one part, but they behave as twelve different springs.
That gap between the drawing and the felt behaviour is where most complaints about custom silicone keypads begin. The usual response is to blame hardness, order a softer compound, and discover that four keys improved while three got worse. Hardness is one variable in a system that also includes membrane geometry, how the sheet sits in the housing, the air trapped underneath, and the point where a carbon pill meets its pad.
Why Do Some Buttons Feel Different on the Same Silicone Keypad?
Feel is not a material property. It is the sum of four resistances the finger meets in sequence: the stiffness of the keytop wall, the bending of the membrane around the key, the volume of air that has to move out of the way, and finally the snap of the dome or the compression of the contact. Change any one of them and the same compound delivers a different press.
Differences in Key Size and Silicone Membrane Geometry
A keypad is not a plate with buttons glued on. It is a perforated sheet, and every hole changes how the material around it moves. A 12 mm key with a 1.2 mm wall does not behave like an 8 mm key with the same wall, because wall stiffness scales with the cube of thickness but only linearly with diameter. Two keys poured from the same batch can therefore differ by a factor that no durometer reading will show.
The land between keys matters as much as the keys. A narrow land acts as a hinge and lets neighbouring keys share the load; a wide land isolates each key but stiffens the whole sheet. When a layout mixes a large Enter key beside small function keys, the large key usually ends up with a thicker wall and a wider land, and it reads as heavier even though the material is identical.
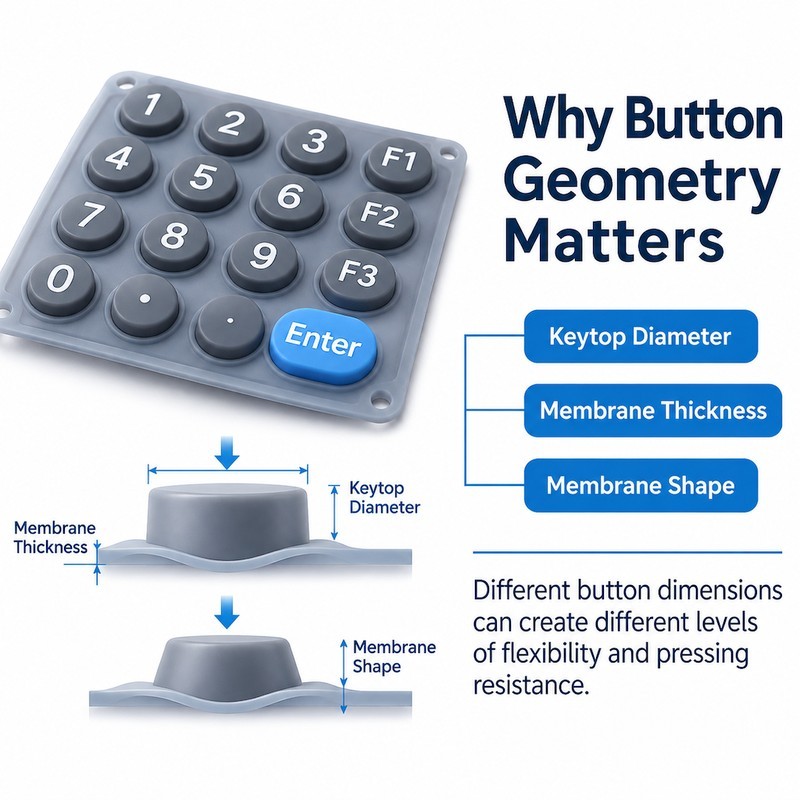
Cut a keypad through the middle and the reason for uneven feedback is usually visible in a single section: one key with a thick, almost vertical wall, its neighbour with a thin wall that merges into the land at a generous radius. The thin one flexes early and feels light; the thick one resists until the dome takes over and then feels abrupt.
The practical fix is rarely a new compound. It is proportion: keeping the ratio of wall thickness to keytop diameter inside a narrow band across the whole layout, and keeping the base radius consistent so that each key starts to bend at a similar point in its travel.
How Button Position Affects Pressing Force
Corner keys behave differently from centre keys for a reason that has nothing to do with the mold. The flange of the keypad is clamped by the housing, and the clamp load travels into the sheet. A key 6 mm from the flange sits in a stiffer region than a key 30 mm away. On a scale with a rubber gasket behind the panel, that preload can be high enough to add noticeable resistance to the outer row.
Support underneath matters just as much. If the PCB stands on three posts instead of four, or if a ribbon connector lifts one corner of the board by a fraction of a millimetre, the key above it has less over-travel before contact. The finger reads that as a hard key. This is why a keypad that measures evenly on a fixture can still be complained about in the field: the fixture is flat, the assembled instrument is not.
The Role of Conductive Contacts and Switching Structures
Mechanical feel and electrical response are separate events that the operator experiences as one. A carbon pill can travel 0.4 mm past the point where the finger has already decided the press is complete. If the pill is small relative to the pad, or offset by a few tenths, the key feels normal and still registers intermittently, which is the most confusing complaint of all.
Pill diameter, pad diameter, the gap between them and the flatness of the pill face all set the point of electrical make. On keys with a moulded dome, the snap is what the finger feels; on flat membrane keys, the contact compression is most of the feedback. Comparing the two on one panel without accounting for that difference will always produce a misleading result.
Which Design Factors Commonly Cause Uneven Tactile Feedback?
| What the operator reports | Most likely origin | First thing to check |
|---|---|---|
| One key heavy, neighbours light | Wall thickness or land width differs across the layout | Section the keypad through both keys |
| Outer row harder than centre | Flange clamp load or gasket preload | Press the same keypad outside and inside the housing |
| Key returns slowly, feels sticky | Trapped air with no vent path | Look for a vent groove or a pierced membrane |
| Feels right, registers unreliably | Carbon pill offset or too small for the pad | Contact resistance across ten presses |
| First batch good, later batch soft | Cavity wear, flash at the land, cure drift | Dimensional report per cavity |
Inconsistent Membrane Thickness Across Different Buttons
Membrane thickness is the quietest variable in the whole part. A difference of 0.15 mm across a panel is invisible on a drawing and obvious to a thumb. It changes local stiffness roughly in proportion to the cube of the thickness, so a small drift in one region can move press force much more than the same drift spread over the whole sheet.
Thickness usually drifts where the material has furthest to flow: at the end of a long keypad, around a large cut-out for a display, or between two rows of tightly packed keys. The mold can be perfectly machined and still produce a gradient if the cavity fills from one edge and the press closes before the last region is packed.
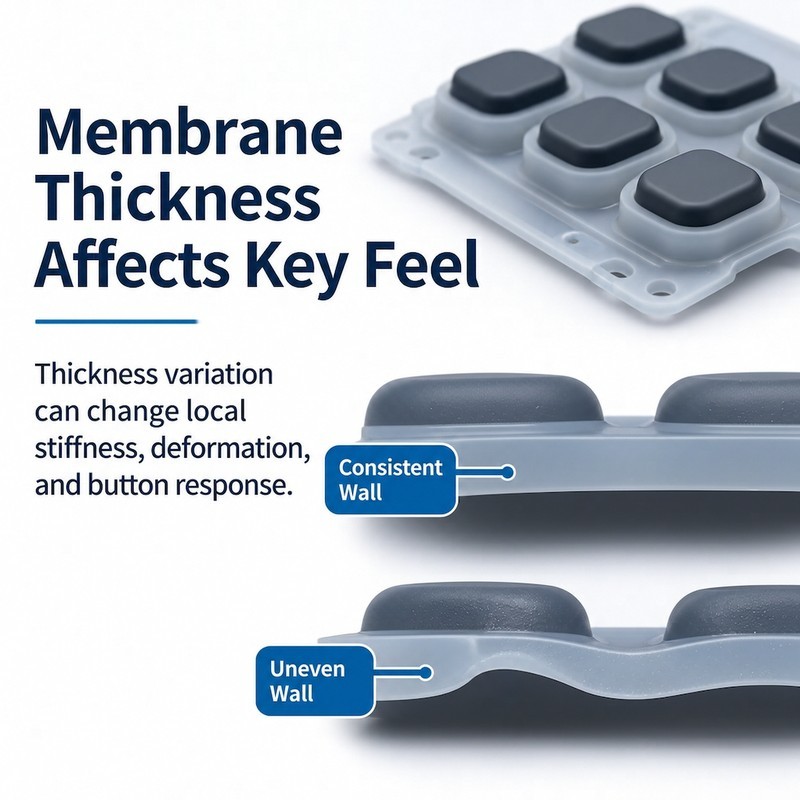
The check is cheap and does not need a laboratory: cut three sections from the first, middle and last cavity of a trial run, measure the membrane wall at the same landmark on each, and compare. If the spread is wider than the dimensional tolerance on the drawing, the press parameters or the cavity layout need attention before the tool is signed off.
Where wall thickness has to vary by design, for example a thin web around a light function key and a heavier web under Enter, the variation should be written on the drawing rather than left to the toolmaker. Unwritten variation becomes uncontrolled variation.
Incorrect Silicone Hardness for the Keypad Structure
Shore A hardness, measured on the scale defined in ASTM D2240, describes how a flat test piece resists an indentor. It does not describe how a 10 mm dome with a 1.1 mm wall will feel. Two compounds at 50 Shore A can differ by 30 percent in press force once they are formed into the same geometry, because hardness and modulus are related but not identical, and because compression molding changes the skin.
Choosing hardness first and geometry second is the usual order, and it is backwards. Geometry decides which part of the press the finger feels; hardness decides how much of it. A panel that needs a light touch for numeric keys and a deliberate press for a destructive function such as a calibration reset can be built from one compound if the two keys are given different walls and different dome heights.
Mold Cavities and Manufacturing Variations
Cavity-to-cavity variation shows up as a trend across a panel rather than a random fault. If keys in the left half of every fourth part feel heavier, look at how those cavities fill and where the parting line sits, not at the compound. Flash at the land is especially misleading: a hairline of flash stiffens the membrane locally and makes a key feel as if it has a thicker wall.
Not every complaint starts in the mold, though. Cure drift, storage of the compound, and the way parts are stripped and trimmed all leave marks on feel. A useful discipline is to record press force on the first, middle and last parts of a run, so that a field complaint can be compared against the batch that produced it instead of against memory.
How Can Manufacturers Improve Button Feedback Consistency?
Optimize Membrane Thickness and Button Geometry
Consistency is a layout problem before it is a material problem. Balance the keys as a group: adjust wall thickness where a key is too light, adjust dome height where it is too abrupt, and keep the land width uniform so that no key is hinged to its neighbour. Changing one key in isolation usually moves the problem rather than solving it, because the sheet redistributes the load.
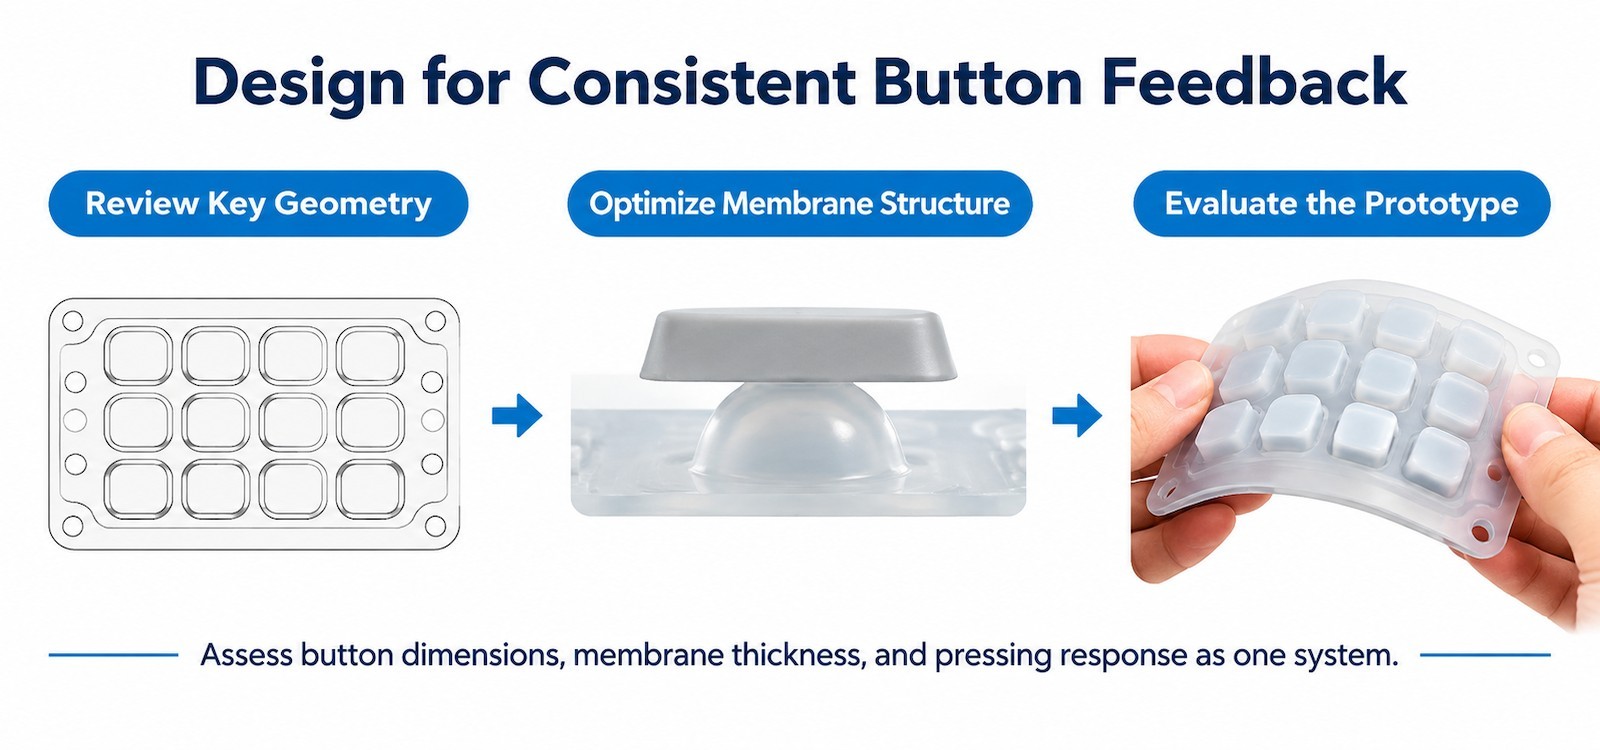
- Review key geometry. Check keytop diameter, wall thickness and the land width around every key, and compare them across the layout rather than key by key.
- Optimize membrane structure. Set dome height and membrane thickness so that the press curve starts at a similar point on every key of the same size class.
- Evaluate the prototype. Measure breakaway force, travel at make, return force and contact resistance with the keypad clamped in its housing.
Where a panel carries keys of very different sizes, it helps to design each size class as a family: one wall ratio for the 12 mm keys, one for the 8 mm keys, one for the 5 mm function keys. Within a class the press forces will then track each other, and the operator reads the difference between classes as intentional hierarchy rather than as a fault.
Select Silicone Hardness Based on Actual Operating Requirements
The right question is not "which hardness feels best" but "what has to be true when the operator is wearing a glove and pressing with a thumb at an awkward angle". A softer compound widens the contact patch and lowers breakaway force, which helps gloved use, but it also lengthens rebound and can make a key feel vague on a fast numeric sequence.
Prototype two hardness options on the same geometry rather than two geometries on the same hardness. Two sets of samples, pressed by the same two or three people, will settle the question faster than any specification table. Our published range for custom keypads runs from Shore A 30 to 80 with key travel of 0.8 to 1.5 mm and actuation force of 150 to 400 g, and within that window the geometry usually deserves more of the attention than the number.
Verify Mechanical and Electrical Performance Together
Measure four things on every key: breakaway force, travel at make, return force and contact resistance. Breakaway force alone hides the difference between a key that resists and then snaps and a key that resists all the way down. Contact resistance alone hides a key that works electrically but feels dead.
Test the complete assembly, not the bare part. Clamp the keypad into the housing, fit the PCB, and repeat the measurements at the corners and the centre. The difference between the free and installed numbers is the preload the design has to live with, and it is often bigger than the difference between two compounds.
What Should Industrial Scale Manufacturers Confirm Before Ordering Custom Silicone Keypads?
Provide Button Layout and Housing Dimensions
Send the key layout with centre distances, key diameters, key heights and the position of every cut-out. Then send the housing: where the panel seats, how the flange is clamped, where the PCB posts sit, and how much space exists behind the membrane for air. A layout without the housing tells half the story, because half of the feel comes from the clamp.
Define Pressing Force and Feedback Requirements
Separate the keys by function. Numeric entry keys are pressed in sequence and want a short, light travel; a calibration or reset key wants a deliberate press that will not happen by accident. Write the intended difference down, with a target range for each group, and say which keys may share a wall thickness and which may not.
Review Prototype Samples Before Mass Production
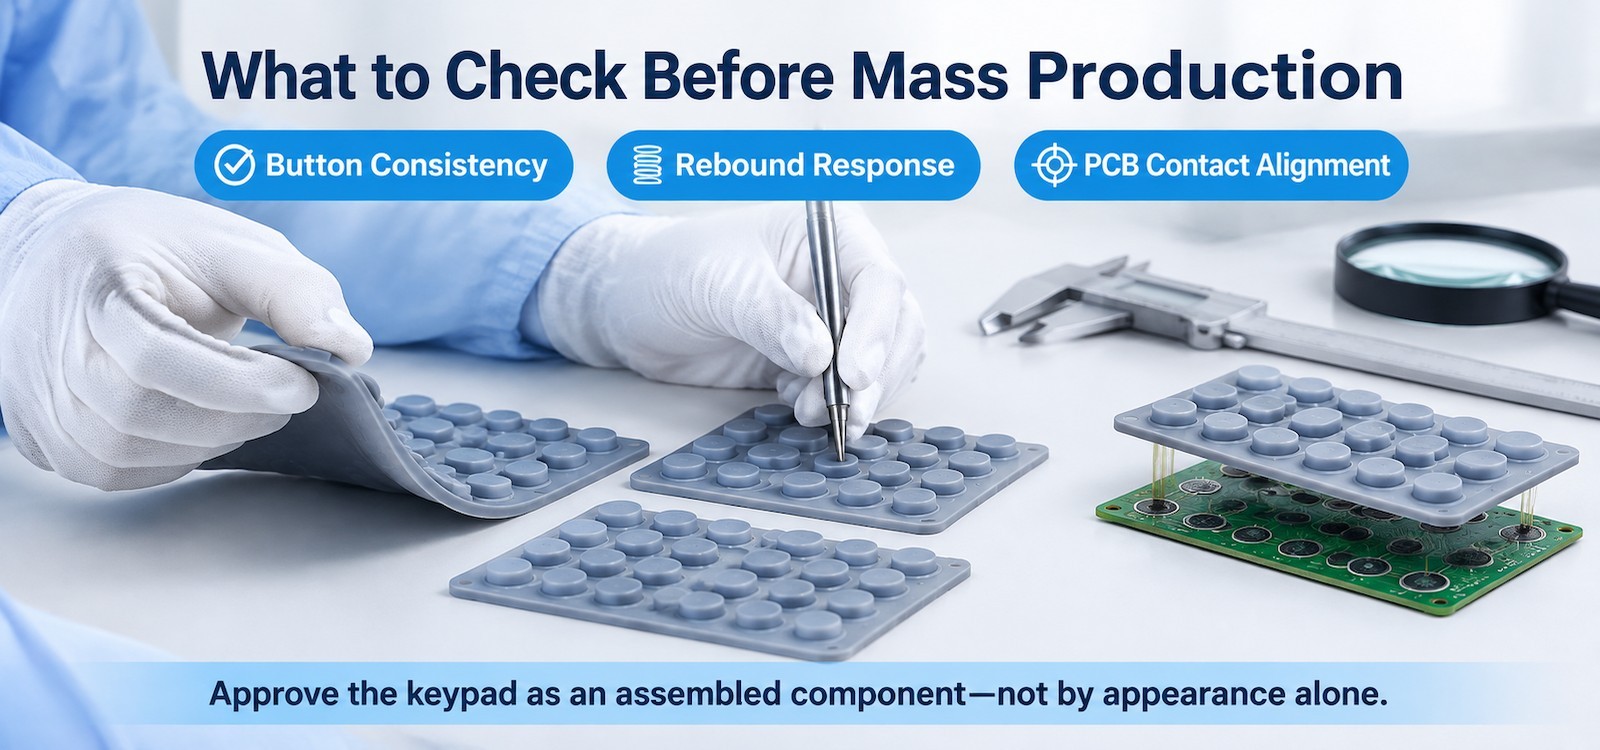
Approve on behaviour, not on appearance. Press every key at least fifty times, note rebound, listen for the change in sound that indicates the dome is collapsing cleanly, and check the electrical make on the same strokes. Then fit the sample into the actual housing and repeat the exercise, because that is the only measurement the end user will ever experience.
Frequently Asked Questions About Uneven Silicone Keypad Feedback
Can different button sizes produce different pressing forces on the same keypad?
Yes. Press force depends on wall thickness, keytop diameter and the land around the key, so a large key and a small key poured from the same compound will not match unless their wall ratios are adjusted. Matching sizes within a class, rather than across the whole panel, is usually the practical answer.
Does softer silicone always provide better tactile feedback?
No. Softer silicone lowers breakaway force and widens the contact patch, which helps gloved operation, but it also slows rebound and can blur the point where a key registers. On numeric panels pressed in fast sequence, a slightly firmer compound often produces a clearer response.
Can membrane thickness adjustments improve button consistency?
They are the most effective single adjustment, because local stiffness changes roughly with the cube of thickness. Evening out the membrane wall across a panel usually brings press forces closer than a compound change, provided the dome geometry is already consistent.
Why do some silicone keypad buttons feel harder near the edges?
The flange is clamped by the housing, and clamp load travels into the sheet, so keys close to the edge sit in a stiffer region. Reduced over-travel from an uneven PCB support or a gasket behind the panel has a similar effect. Comparing free and installed press force shows which of the two is responsible.
What should be checked before approving a custom silicone keypad prototype?
Breakaway force, travel at make, return force and contact resistance on every key, measured in the housing rather than on the bench. Add a section through the membrane at both ends of the part to confirm wall thickness is even, and press each key fifty times to look for drift. Our notes on keys that feel harder than their neighbours cover the same checks in a different application.
What This Means for a Scale Builder
Consistent feedback comes from treating the keypad as a structural part: a sheet with a stiffness map, clamped into a housing, venting air, closing contacts at a defined point. Compound choice sits inside that system, not above it. When a panel is designed with even wall ratios, a defined vent path, and a contact geometry matched to the pad, hardness becomes a fine adjustment rather than a rescue operation.
FromRubber is operated by Dongguan Bohao Electronic Technology Co., Ltd. in Dongguan, Guangdong. FromRubber moulds custom keypads in Dongguan across 32 vacuum and flat-bed hydraulic presses, with seven CNC machines in house for cavity and electrode work, under IATF 16949:2016, ISO 9001:2015 and ISO 14001:2015. Most of the uneven-feedback cases we see are settled at the drawing stage, before a mold is cut. If you have a layout that already has a difficult key, send the drawing and the housing section and we will tell you which keys are likely to feel different, and why.
Talk to the people who cut the cavity
Send your keypad drawing, housing section and target press forces. Phone, WhatsApp or WeChat: +86 18676210913. Drawings can also be uploaded through the contact page.
Related Reading
Sources and Test Methods Referenced
- ASTM D2240-15(2021), Standard Test Method for Rubber Property, Durometer Hardness. ASTM International.
- ISO 37:2017, Rubber, vulcanized or thermoplastic, determination of tensile stress-strain properties. ISO.
- ISO 23529:2016, Rubber, general procedures for preparing and conditioning test pieces for physical test methods. ISO.
- ASTM D395-18(2025), Standard Test Methods for Rubber Property, Compression Set. ASTM International.
- FromRubber product data for custom silicone rubber keypads: hardness range, key travel and actuation force as published on the Custom Silicone Rubber Keypad page.
- Editions checked against the ASTM, ISO and IEC publisher listings in November 2026.